Pakistan: +92 321 4466539 China: +86 131 2867 6504 hassanplas@gmail.com
HassanPlas Tooling

PET Preform Moulds

Hot-runner PET preform moulds from 2 to 96 cavities for mineral water, carbonated drinks, juice, edible oil, jars and 5-gallon bottles. We design them to your preform weight and neck finish, build them for your machine, and trial them before shipment.

Built for long, stable runs

Preform moulds that hold weight and cycle

  • Balanced hot runner, valve-gate or open-gate, for even fill and consistent preform weight across every cavity.
  • Self-locking taper cavity-and-core alignment for concentric walls and long mould life.
  • Efficient cooling close to the cavity surface for short cycle times and low AA (acetaldehyde) generation.
  • Stainless cavities and cores with a high polish for clear preforms and corrosion resistance.
  • Interchangeable inserts: neck rings, cores and cavities can be swapped to change neck or weight.
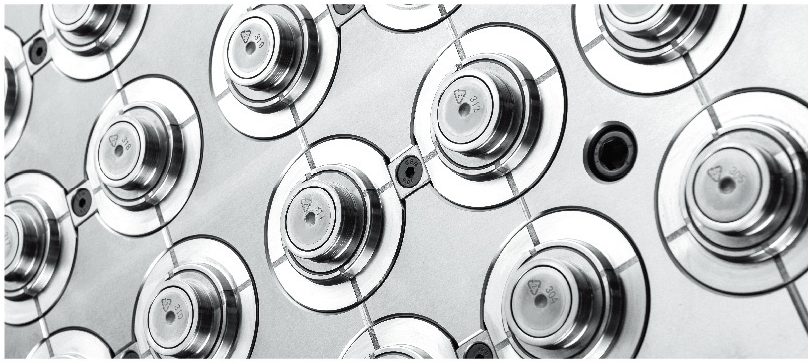
Multi-cavity PET preform mould cavity plate

Neck finishes & typical applications

Neck finishTypical useTypical cavitation
PCO 1881Carbonated soft drinks, water (short, lightweight neck)16–72
PCO 1810CSD and water (traditional neck)16–72
29/25 · 30/25Still mineral water, lightweight24–96
38 mmJuice, dairy, hot-fill, edible oil8–48
48 mm · wide mouthJars, edible oil, food4–32
55 mm5-gallon / 18.9 L water bottles2–8

Cavitation ranges are typical and depend on preform weight, machine platen and shot size. We confirm the exact number with your machine.

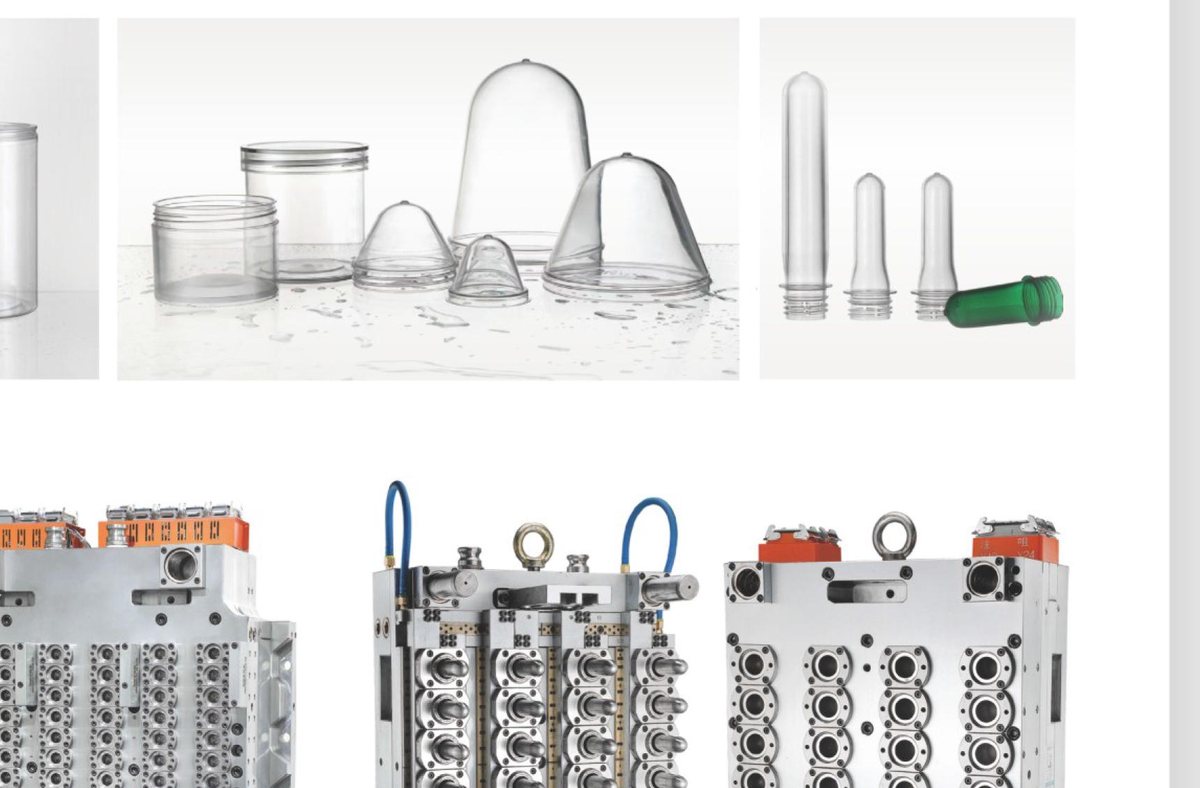
PET preforms, jars and high-cavity preform moulds

What you get with every preform mould

01

Preform design

Preform drawing optimised for your bottle: weight, wall thickness and stretch ratios checked against the blow mould.

02

Machine fit

Built to your machine's platen, tie-bar, ejector and robot take-out plate, whether it is a HassanPlas machine or another brand.

03

Trial & samples

Trialled on a preform machine, with samples and a weight and dimension report before shipment.

04

Spare parts kit

Recommended spare neck rings, cores, nozzle tips and heaters, so wear doesn't stop your line.

Pair with: PET preform injection machines · PET blow moulding machines · Preform mould buying guide

Frequently asked questions

How many cavities should my preform mould have?

Cavitation follows from your target output, preform weight and machine size. Small water preforms commonly run on 24–72 cavity moulds on mid-size machines, and heavy 5-gallon preforms run on 2–8 cavities. HassanPlas sizes the cavitation together with the preform injection machine.

Which neck finishes do you make?

PCO 1810 and PCO 1881 (water and CSD), 29/25 and 30/25 lightweight water necks, 38 mm, 48 mm and wide-mouth jar necks, and 55 mm for 5-gallon bottles. Custom neck finishes can be built from your drawing.

Do the moulds fit my existing preform machine?

Yes. We build the mould to your machine's platen size, tie-bar distance, ejector layout, nozzle and robot take-out. Send us the machine model and mould-mounting drawing.

What steel is used?

Cavities and cores are made in stainless mould steel for corrosion resistance and polishability, neck rings in hardened tool steel, and plates in pre-hardened or stainless steel. Exact grades are listed in your quotation.

Get a preform mould quote

Send your preform weight, neck finish, cavity count and machine model, or a sample bottle. We'll design the preform and quote the mould. WhatsApp +92 321 4466539.

Request a Quote →
WhatsApp