This plastic machine installation checklist is the one we send to buyers while their machine is still at sea. The machine itself is usually the easy part. What delays start-up is the factory around it: a main switch that is too small, compressed air at the wrong pressure, a chiller that cannot hold mould temperature in summer, or no crane to lift the clamping unit off the truck. Every one of those can be fixed in advance, cheaply, and almost none of them can be fixed quickly once the technician is standing in your hall.
The checklist applies to injection moulding machines, PET blow moulding machines, extrusion blow moulding and most other plastic processing equipment. Always follow the manufacturer's foundation drawing and utility data sheet for your specific model; this guide tells you what to ask for and what to check.
Why preparation decides your start-up date
A commissioning technician typically comes for a fixed number of days. If the factory is ready, those days go into setting up the mould, tuning the process and training operators. If it is not, they go into waiting for an electrician, and you either pay for extra days or the technician leaves before your operators are confident. Ask your supplier, or HassanPlas if we are handling your project, for the utility requirements sheet as soon as the contract is signed. It should state:
- Machine footprint, weight and the heaviest single lift
- Installed electrical power, voltage, frequency and recommended main breaker
- Compressed air pressure and consumption
- Cooling water flow, temperature and pressure for the machine, mould and oil cooler
- Any foundation or anchoring requirement
Floor, foundation and ceiling height
Most small and medium injection and blow moulding machines stand on a sound, level industrial concrete floor using anti-vibration levelling mounts, without a special foundation. Large machines, high-speed machines and long extrusion lines may need a dedicated reinforced pad, sometimes isolated from the surrounding slab. The manufacturer's drawing is the authority.
- Level: the floor must be level across the machine footprint so the machine can be trued with its levelling pads. A badly out-of-level floor causes tie bar and platen problems on injection machines and alignment problems on blow moulders.
- Load: check the floor can carry the machine weight plus mould weight, concentrated on its feet. If in doubt, ask a structural engineer.
- Pits and trenches: plan cable and pipe trenches before pouring concrete; cutting them afterwards is expensive.
- Ceiling height: allow space above the machine for mould changes by crane or hoist, and for the hopper loader on top of the barrel. Tall machines such as some extrusion blow moulders and vertical machines need extra headroom.
- Curing time: new concrete needs time to cure before carrying a heavy machine. Pour early.
HassanPlas tip: Mark the machine outline, including the mould area, safety gates and maintenance access, on the floor with paint before the container arrives. It immediately shows whether the space really works.
Unloading and moving the machine
Decide in advance how each crate will come off the truck and onto its final position. Check the packing list for the heaviest piece.
- An overhead crane is ideal. If you do not have one, book a mobile crane with enough capacity and reach, and confirm site access for it.
- Forklifts must be rated for the weight at the load centre of the crate, not just the nominal weight. Long machines may need two forklifts.
- Have skates, rollers, jacks and lifting slings of the right rating available for final positioning.
- For open-top or flat rack containers, the crane must lift from above at the delivery point.
- Check door widths and heights along the route from the truck to the machine position.
Power supply sizing
Electrical supply is the most common cause of delayed start-up. Work with a qualified electrician using the machine's data sheet.
Main switch and cable
For a three-phase load, current is roughly the power divided by (1.732 × voltage × power factor). As a worked example, a machine drawing 100 kW at 400V with a power factor of 0.85 draws about 170 A at full load. The electrician then selects a main breaker and cable cross-section with appropriate margin for that current, the cable length, the installation method and the local electrical code. Remember to add the auxiliary equipment: chiller, dryer, loader, compressor, mould temperature controller and conveyors often add a significant share to the line's total load.
Voltage and frequency
Confirm the machine was built for your supply: for example 380V/50Hz, 400V or 415V/50Hz, or a 60Hz supply such as 220V, 440V or 480V. If it was not, a transformer may be needed. Check the nameplates on arrival.
Voltage stability
Where grid voltage fluctuates or drops under load, controllers, servo drives and heaters suffer. Measure your supply at different times of day before installation. Depending on the readings, you may need a voltage stabiliser, a dedicated transformer, or power-factor correction. If you rely on a generator, size it for the starting current of motors and compressors, not only running load.
- Dedicated distribution board for the line, with separate breakers per machine
- Proper earthing, tested and documented
- Isolator within reach of each machine
- Supply terminated near the machine's electrical cabinet, ready for connection
Compressed air: low pressure and high pressure
Compressed air requirements vary more between machine types than any other utility, and confusing them is a classic mistake.
| Machine type | Typical air pressure | What it is used for | Notes |
|---|---|---|---|
| Injection moulding | Low pressure, typically 6–8 bar | Mould blow-off, air valves, robots, pneumatic gates | Consumption usually modest; check robot and mould requirements |
| Extrusion blow moulding | Low pressure, typically 6–10 bar | Parison blowing, pneumatic movements | Larger containers and multi-cavity heads use more air |
| PET stretch blow moulding | High pressure, commonly 25–40 bar for blowing | Pre-blow and final blowing of bottles | Needs a high-pressure compressor plus a separate low-pressure supply for actuators |
| Injection blow moulding | Low to medium pressure; check data sheet | Blowing and actuators | Consumption depends on cavities and container size |
For PET lines in particular, size the high-pressure compressor on the machine's stated consumption at full output, plus a margin, and plan for future cavity increases. A complete compressed air system should include:
- Compressor of the right pressure class and capacity
- Air receiver to buffer demand peaks, rated for the pressure
- Refrigerated dryer to remove moisture, which otherwise damages valves and marks bottles
- Filters (particle and oil) suited to the application, especially for food and beverage containers
- Piping of adequate diameter with minimal pressure drop, and drain points at low spots
Common mistake: Buying a PET stretch blow moulding machine and assuming the factory's existing 8-bar compressor will do. It will not. The high-pressure compressor is a separate, significant purchase and should be in the budget from day one.
Cooling water, chillers and cooling towers
Cooling determines cycle time. An undersized chiller shows up in hot months as longer cycles, warped parts and hydraulic oil overheating.
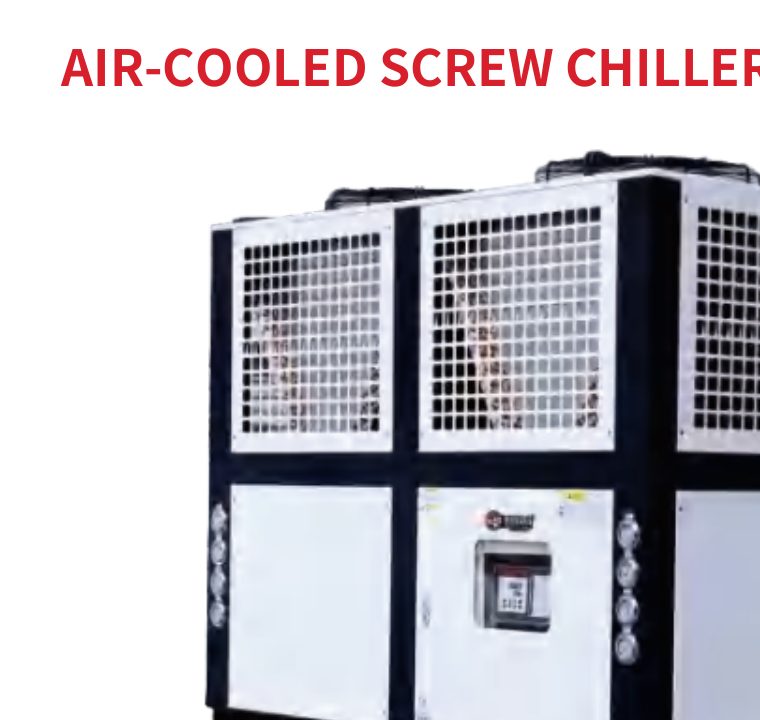
- Chiller: provides chilled water, typically for mould cooling. Size it from the cooling load given by the machine and mould supplier, add a margin for your hottest ambient temperature, and consider future moulds. Air-cooled chillers are simpler; water-cooled chillers are more efficient but need a cooling tower.
- Cooling tower: often used for the hydraulic oil cooler, barrel feed throat and water-cooled chillers, where water a few degrees above ambient is sufficient.
- Water quality: hard or dirty water scales mould channels and heat exchangers. Use treated or softened water, filtration, and a closed loop where possible.
- Piping: insulated chilled water lines, adequate diameter, isolating valves and a bypass at each machine, and flexible hoses for connection.
- Mould temperature controllers for processes that need warm rather than chilled moulds.
Chillers, cooling towers and mould temperature controllers are all available through our auxiliary equipment range, sized to match the main machine.
Material handling and ventilation
Most plastics need some combination of drying, conveying and mixing before they reach the barrel.
- Dryer: PET, PC, PA and other hygroscopic materials must be dried properly; PET preform production typically uses a dehumidifying dryer. Size it on throughput and residence time.
- Loader: vacuum loaders move material from bags or silos to the hopper; position power and air for them.
- Mixer and dosing: for masterbatch and regrind, plan where the mixer sits and how material reaches it.
- Granulator: for in-house regrind of runners and rejects, placed close to the machine.
- Storage: dry, covered storage for raw material bags, off the floor.
Moulding halls get hot from heaters, motors and hydraulic systems. Plan for ventilation or extraction above the machines, and keep the area around chillers and electrical cabinets within their rated ambient temperature. Very high ambient temperatures reduce chiller capacity and shorten electronics life.
Layout, flow and safety
Lay out the line in the order material flows: raw material storage, drying and conveying, the machine, downstream equipment (conveyor, robot, leak tester, packing), then finished goods. Avoid crossing routes for forklifts and people.
- Leave maintenance access on all sides, including space to pull a screw from the barrel on injection machines
- Allow mould change access for the crane or forklift
- Keep electrical cabinets away from water lines and give them clearance for doors to open
- Install fire extinguishers suitable for electrical and plastics fires near each line
- Provide guarding and interlocks as supplied; never bypass safety gates
- Provide PPE: heat-resistant gloves, eye protection, hearing protection near granulators and compressors
- Mark walkways and forklift routes on the floor
Plastic machine installation checklist for technician arrival
Confirm every item below before the technician travels. Send photos to your supplier as evidence.
| Item | Ready when |
|---|---|
| Machine and auxiliaries positioned | Unpacked, on final position, roughly levelled |
| Power | Correct voltage measured, cable terminated at the cabinet, breaker sized and labelled |
| Compressed air | Correct pressure at the machine, dryer and filters running |
| Cooling water | Chiller and tower running, lines flushed, flow confirmed |
| Hydraulic oil | Correct grade and quantity on site, per manual |
| Raw material | Enough for trials, already dried where needed |
| Mould and preforms | On site, cleaned, with any inserts and spares |
| Lifting equipment | Crane or hoist available for mould mounting |
| Tools | Basic hand tools, multimeter, spirit level, torque wrench |
| People | Electrician, maintenance fitter and operators assigned for the full visit |
| Technician logistics | Visa, accommodation, transport and interpreter if needed |
Installation timeline, training and spare parts
A realistic sequence for a single machine with its auxiliaries looks like this, though timings vary with machine size and complexity:
- While the machine is in production: receive the utility sheet and foundation drawing; order compressor, chiller and electrical work; pour any foundation.
- While at sea: complete electrical, air and water installation; arrange unloading; apply for technician visa.
- Arrival: unload, position, unpack, inspect for transit damage against the packing list.
- Commissioning: levelling, connections, oil filling, dry running, mould mounting, first shots or bottles, process tuning.
- Production trial and training: continuous running at target output, with operators running the machine under supervision.
- Handover: written settings, maintenance schedule and sign-off against the acceptance criteria.
Training should cover daily operation, start-up and shutdown, mould change, basic troubleshooting, and preventive maintenance for both operators and maintenance staff. Ask for settings records and photographs so knowledge does not leave with one operator.
Spare parts starter kit
Keep a starter kit on the shelf from day one. Typical items include heater bands, thermocouples, fuses, relays and contactors, proximity switches, seals and O-rings, solenoid valve coils, filters and, for PET lines, blowing valve seals and lamp sets. Ask for a recommended list for your model. HassanPlas dispatches further spare parts from China when needed.
If you are planning a complete new plant rather than a single machine, our guide to starting a PET bottle manufacturing plant covers the wider planning. For installation, commissioning and operator training by technicians, see our services.
Frequently asked questions
Does an injection moulding machine need a special foundation?
Most small and medium injection moulding machines stand on a level, sound industrial concrete floor using levelling mounts. Large or high-speed machines may need a dedicated reinforced foundation. Always follow the manufacturer's foundation drawing for your model.
What air pressure does a PET blow moulding machine need?
PET stretch blow moulding typically needs high-pressure air, commonly in the 25 to 40 bar range, for blowing, plus a separate low-pressure supply for actuators. Check the exact pressure and consumption on your machine's data sheet and size the compressor, receiver, dryer and filters to suit.
How do I size a chiller for a plastic moulding machine?
Use the cooling load stated by the machine and mould supplier, add a margin for your hottest ambient temperature and for future moulds, and choose between air-cooled and water-cooled designs based on your site. Undersizing shows up as longer cycles in hot months.
How do I size the main breaker and cable?
Add up the installed power of the machine and all auxiliaries, calculate full-load current for your voltage, and have a qualified electrician select the breaker and cable cross-section according to cable length, installation method and local electrical code.
Do I need a voltage stabiliser?
If your supply voltage fluctuates or drops under load, a stabiliser or dedicated transformer protects controllers, servo drives and heaters. Measure the supply at different times of day before installation to decide.
What should be ready before the commissioning technician arrives?
The machine positioned, power connected at the correct voltage, compressed air and cooling water running, hydraulic oil, dried raw material, the mould, lifting equipment, basic tools, and an electrician, fitter and operators assigned for the whole visit.
Want a utility checklist for your machine?
Tell HassanPlas which machine you are buying and we will send its power, air and water requirements, and quote auxiliaries and installation. WhatsApp +92 321 4466539, China +86 131 2867 6504, or email hassanplas@gmail.com. Landed-cost quotes within 48 hours.
Request a Quote →